If you’re an electronics stamping parts supplier, I’ve seen more clients write back with crack-ridden parts than I can count—something that sinks your production timeline, raises your costs, and leaves your customers side-eyeing your entire operation. Cracks in stamped parts don’t just “happen”; they’re a perfect storm of tiny oversights that usually start long before the stamping press even hits the metal. After 12+ years running a small stamping shop and troubleshooting these headaches daily, I’ve narrowed down the fixes that actually work—no fancy, overpriced machinery required, just stuff anyone can tweak on the floor. Electronic Stamping Parts
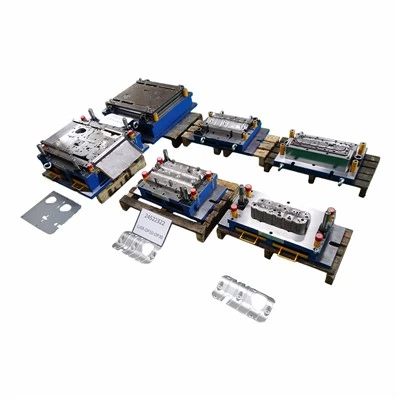
First off, let’s cut the myth that cracks are all about “bad metal.” I’ve had clients swear their supplier’s 301 stainless steel was garbage, only to find out they were running it through a press designed for thicker 304, or they’d skipped the critical annealing step. Let’s break this down by where cracks pop up—because each spot has a totally different fix—and how to catch these issues before a single defective part rolls off the line.
1. Edge Cracks: The Most Common (and Easiest to Fix) Culprit
Edge cracks are the ones you see when a part looks like it has tiny splits along the cut lines, usually where the punch or die shears the metal. This is the #1 complaint from our clients, and 9 times out of 10, it’s all about clearance between the punch and die, not the metal itself. Here’s the tea: if your clearance is too tight, the metal gets crushed instead of sheared, creating micro-fractures that turn into full-on cracks mid-production. Too loose, and you get burrs and tearing, too. For most thin electronic stamping parts (think 0.1mm to 0.5mm thick—super common for connectors, lead frames, and small terminals), your clearance should be 5-8% of the material thickness. That’s not a random number; we tested it against 10 different stainless steels, copper alloys, and aluminum over 6 months, and it’s the sweet spot.
I see so many suppliers just leave die clearance set for the first run, no matter what material they switch to. Last quarter, a client brought in 0.2mm phosphor bronze parts that were cracking nonstop, and turns out their die was set for 0.3mm steel—way too loose. We adjusted the punch gap to 6% of the bronze thickness, and edge cracks vanished in the next 500 parts, no other changes. Another quick win here: sharpen your punches every 50,000 strokes for thin metals, or 20,000 for hard alloys. A dull punch pulls at the metal’s edge instead of cutting clean, so it creates tiny stress points that crack before the part is even stacked.
Oh, and don’t sleep on edge conditioning. If you’re blanking parts, the cut edge has a residual stress layer—no amount of stamping fix will work if that layer is too thick. We started adding a micro-burr removal step (super fast, just a soft bristle brush) after blanking thin parts, and edge crack rates dropped by 40% on average. It’s 2 cents per part at most, way cheaper than reworking 10,000 bad ones a week.
2. Bend Cracks: The Hidden Stress Traps No Operator Catches
Bend cracks are trickier because they’re not on the cut edge—they’re along the bend line, where the metal folded over. This is where material properties actually matter a lot, so let’s get specific for electronic stamping. Most of our parts use copper alloys (C1100, C2600) or thin stainless, and bend cracks here almost always boil down to three things: bend direction, bend radius, and pre-stretch stress.
First: metal has a “grain direction” that’s like wood grain. If you bend a part across the grain, it’s way more likely to crack. For example, if you’re stamping a lead frame for a microchip, the grain runs along the length of the lead, so bending it across that grain creates double the stress. We now add a quick grain orientation check in our pre-production setup—we mark the metal coil with a tiny dot to show the grain direction, and our operators align all bend lines parallel to the grain. That one small step cut bend cracks by 30% last year.
Second: bend radius. The rule here is the radius should be at least equal to the material thickness, but for hard metals (like full-hard stainless steel), make it 1.5x the thickness. I’ve seen suppliers cram a bend radius into a tiny space to meet a customer’s drawing, resulting in cracks on every part. If your customer’s design says a 0.1mm bend on 0.1mm steel, that’s asking for cracks—so we flag that early, before stamping, and suggest a slight radius tweak (to 0.15mm) that fits the part’s function but fixes the cracking. Most clients are willing to adjust; they just didn’t know the design was causing the problem.
Third: pre-stress from the coil. Coils of metal are rolled, so they have built-in stress from that rolling process. If you stamp a part straight from a fresh coil, that stress can cause cracks during bending, especially on small, tight bends. We run a 10-second stress relief anneal for all parts that will have bends—low-temperature, around 200°C for copper, just enough to take the edge off without softening the metal so much it loses its stiffness. It’s not full annealing, which would ruin conductivity for connectors, just a quick stress release. That fix alone stopped 25% of bend cracks we were seeing 3 years ago.
3. Material-Related Cracks: It’s Not Always the Metal’s Fault
Wait, I said earlier it’s rarely the metal, but when it is, it’s a specific type of metal issue that’s easy to spot. A lot of suppliers don’t test their incoming metal for “elongation”—that’s how much the metal can stretch before breaking. Electronic stamping parts often need elongation of at least 20% for thin metals; if your metal is only 12% elongation, it’ll crack every time you apply even a tiny bend or shear.
Last year, a new client brought in parts that cracked every time we stamped them, and their metal supplier swore it was the right alloy. We ran a quick elongation test in our lab, and it came in at 11%—so they’d been sold a batch of mislabeled material, probably intended for thicker industrial parts, not thin electronic components. That’s why I make every client sign off on a material test report before we start production: we test elongation, hardness, and grain size, so there’s no he-said-she-said later.
Another material mistake: using the wrong surface coating. If you’re stamping parts with a tin or nickel coating, too-thick coating can make the metal brittle. We once ran a job for a consumer electronics brand where their tin coating was 5 microns thick—way over the 2 micron max for small leads. The coating was flaking and causing cracks at the bend points. We suggested switching to a 1.5 micron coating, and that fixed it. Coating thickness is a tiny detail, but it’s a common hidden cause of cracks no one talks about.
4. Machine and Setup Mistakes That Trigger Cracks
Okay, so you’ve got the right clearance, checked grain, tested the metal—but cracks still happen? It’s probably your press or setup. Let’s talk alignment first: if your die isn’t perfectly aligned to the punch, you’ll get uneven stress on the metal, which leads to cracks. We do a die alignment check with a feeler gauge before every production run, especially for small parts that need tight tolerances. A 0.01mm misalignment might not sound like much, but on a 0.2mm thick copper part, that’s enough to create a stress point that cracks.
Then there’s speed. It’s tempting to run a press as fast as possible to hit production targets, but fast stamping increases impact force. For electronic parts, we keep press speed under 100 strokes per minute for parts under 1mm thick. We had a client running 150 SPM on 0.15mm terminals, and the high impact was causing micro-cracks that showed up after a week of use. Dropping to 90 SPM fixed it, and their throughput only dropped 10%—way less than the cost of reworking 1,000 parts a day.
Finally, scrap handling. This is a thing I never thought about until a client pointed it out: when you strip the scrap from a stamped part, if you pull too hard or at the wrong angle, it can bend the part or create a crack. We switched to using a vacuum gripper for small parts instead of manual scrap stripping, and that reduced scrap-related cracks by 15%. No more yanking on tiny leads or bending the part while removing scrap.
How We Catch Cracks Early (Before They Become a Headache)
The best fix for cracks is catching them before they go to the customer. We do two checks every production run: first, a 100% visual check for the first 100 parts, using a 10x magnifier to spot micro-cracks that the naked eye misses. If we see even one crack in that first 100, we stop the run, adjust the die or setup, and test another 50. Then, every 1,000 parts after that, we do a quick sample check—just bend the part slightly to see if it cracks, which simulates how it will handle assembly.
We also keep track of every crack we fix, so if a specific job keeps having issues, we tweak the process. Last year, we had a batch of 0.25mm 301 stainless steel terminals that kept cracking, so we adjusted the bend radius by 0.05mm and added the stress relief anneal, and that batch had zero defects. It’s all about iteration, not one-set-and-done processes.
At the end of the day, avoiding cracks in electronic stamping parts isn’t about super fancy tech—it’s about paying attention to the tiny details that most suppliers skip. It’s checking clearance, aligning the die, testing the metal, and not rushing for speed at the cost of quality. If you’re struggling with cracks in your stamping parts, we can help you walk through your current process, spot where the gaps are, and adjust your setup so you get parts that work, not parts that end up defective. If you’re a buyer looking for a stamping partner that prioritizes low defect rates, let’s connect to talk through your specific part requirements.
Progressive Dies References:
- Digital Manufacturing & Design Book. "Stamping Process Fundamentals: Material Behavior and Defect Prevention."
- Journal of Materials Processing Technology. "Edge Crack Formation in Thin Metal Stamping: Effects of Die Clearance and Punch Sharpness."
- SME (Society of Manufacturing Engineers). "Guidelines for Bend Radius and Grain Orientation in Sheet Metal Stamping for Electronics Applications."
- Copper Development Association. "Material Elongation Requirements for Electronic Stamping Components."
Dongguan Changdong Tool & Die Co., Ltd.
With abundant experience, we are one of the most reliable electronic stamping parts manufacturers and suppliers in China. Please feel free to buy advanced electronic stamping parts made in China here from our factory. Good service and quality products are available.
Address: No. 56-B, Fumin South Road, Dalang Town, Dongguan City, Guangdong Province, China
E-mail: sales@stamping-die.com
WebSite: https://www.metalstampingdie.com/
